Protein Deaminase for Cheese: Pilot Trials, Process Control and Bulk Supply
Protein deaminase (protein-glutaminase) for cheese plants and dairy ingredient buyers: where to add it, pilot design, defects, QC, cost-in-use and wholesale quotes.
A buyer's guide for cheese manufacturers, processed-cheese and analogue producers, and the dairy ingredient distributors who supply them: what protein deaminase changes in cheese, where it goes in the process, how to run a decision-ready pilot, and what to send for a wholesale quote.
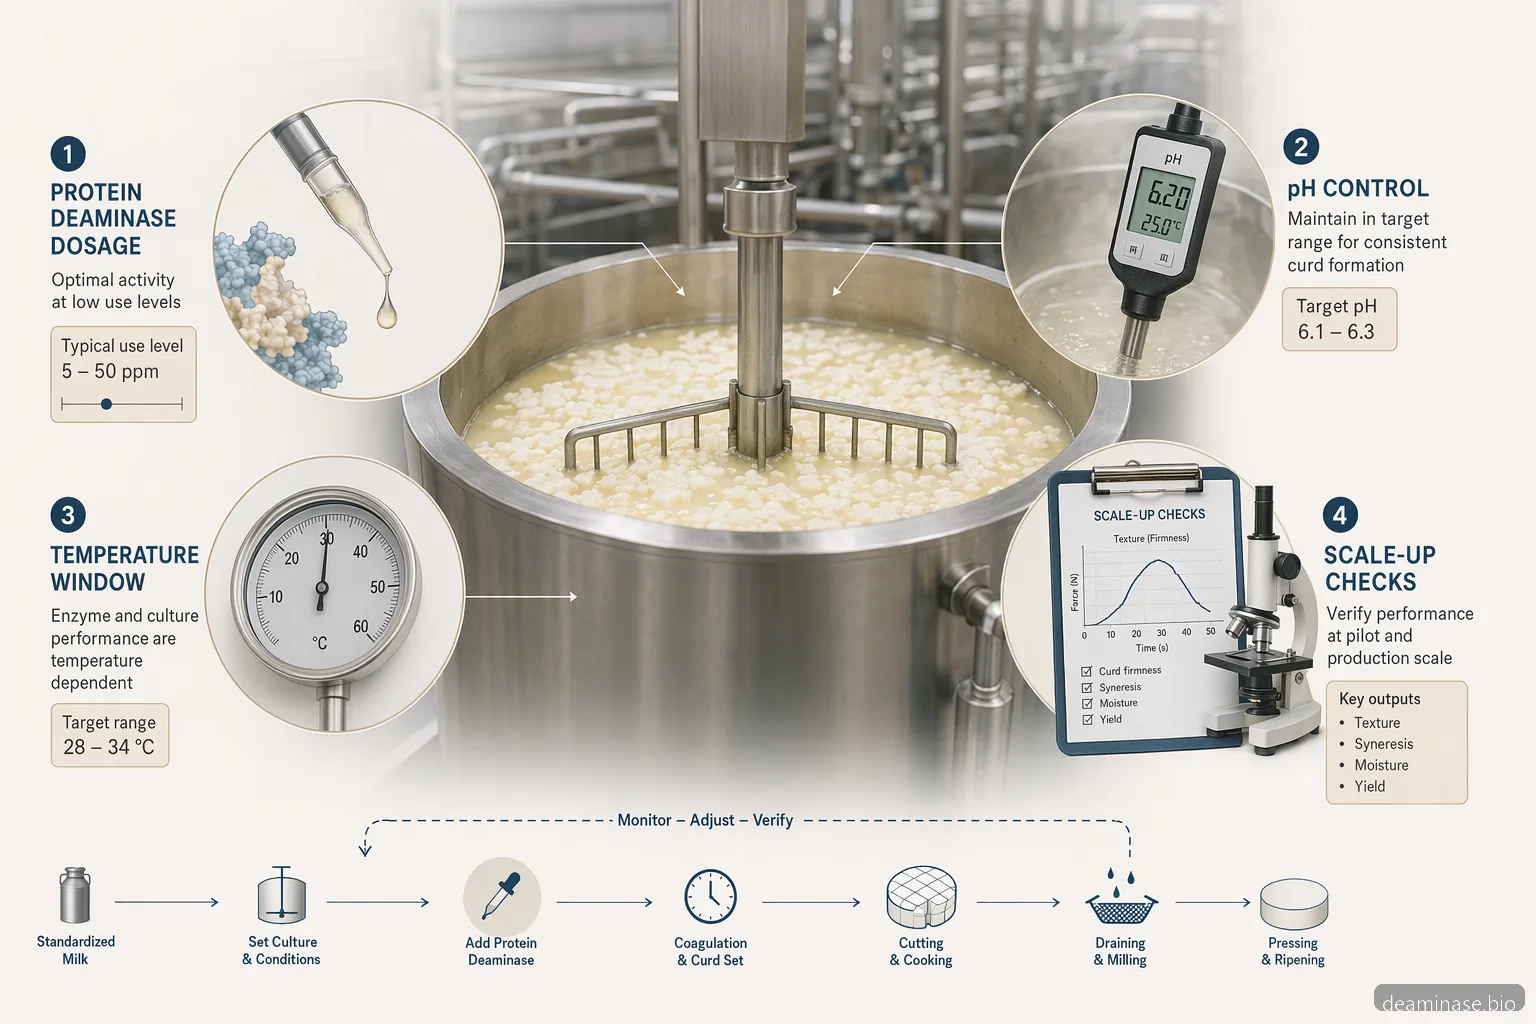
What Protein Deaminase Changes in Cheese
Protein deaminase, often sold as protein glutaminase, converts glutamine residues in food proteins to glutamic acid residues. In cheese systems this changes protein charge, hydration, emulsification and interaction with calcium. The business case is strongest where protein functionality limits yield, sliceability, spreadability, melt or moisture control: processed cheese with inconsistent melt, brittle or variable texture, and cheese analogues or hybrid dairy-plant products whose proteins do not hydrate well. It is not a fix for poor milk quality, wrong pH, calcium imbalance or sanitation problems.
Relevant for dairy cheese, processed cheese, cheese analogues and hybrid dairy-plant systems. • Evaluate it against one defined defect such as poor melt, weak emulsification or texture variation. • Pilot validation comes before production dosing.
Where to Add the Enzyme in a Cheese Process
For industrial protein deaminase cheese work, addition point should match the manufacturing objective. In many trials, protein glutaminase for cheese is added to milk, standardized milk, milk protein concentrate slurry, or a dairy-protein premix before rennet, culture acidification, emulsifying salts, or final cooking. Pre-treatment allows time for protein modification before the curd structure is formed. In processed cheese or cheese analogue systems, the enzyme may be evaluated in a hydrated protein phase before heating and blending with fat, salts, and flavors. If the process includes a later pasteurization or cook step, validate whether it reduces residual enzyme activity. If no kill step is present, confirm residual activity, labeling requirements, and shelf-life behavior with regulatory and quality teams.
Pre-rennet milk treatment can affect curd firmness and whey separation. • Premix treatment is useful for casein, whey, and milk protein concentrates. • Thermal inactivation must be validated in the real product matrix.
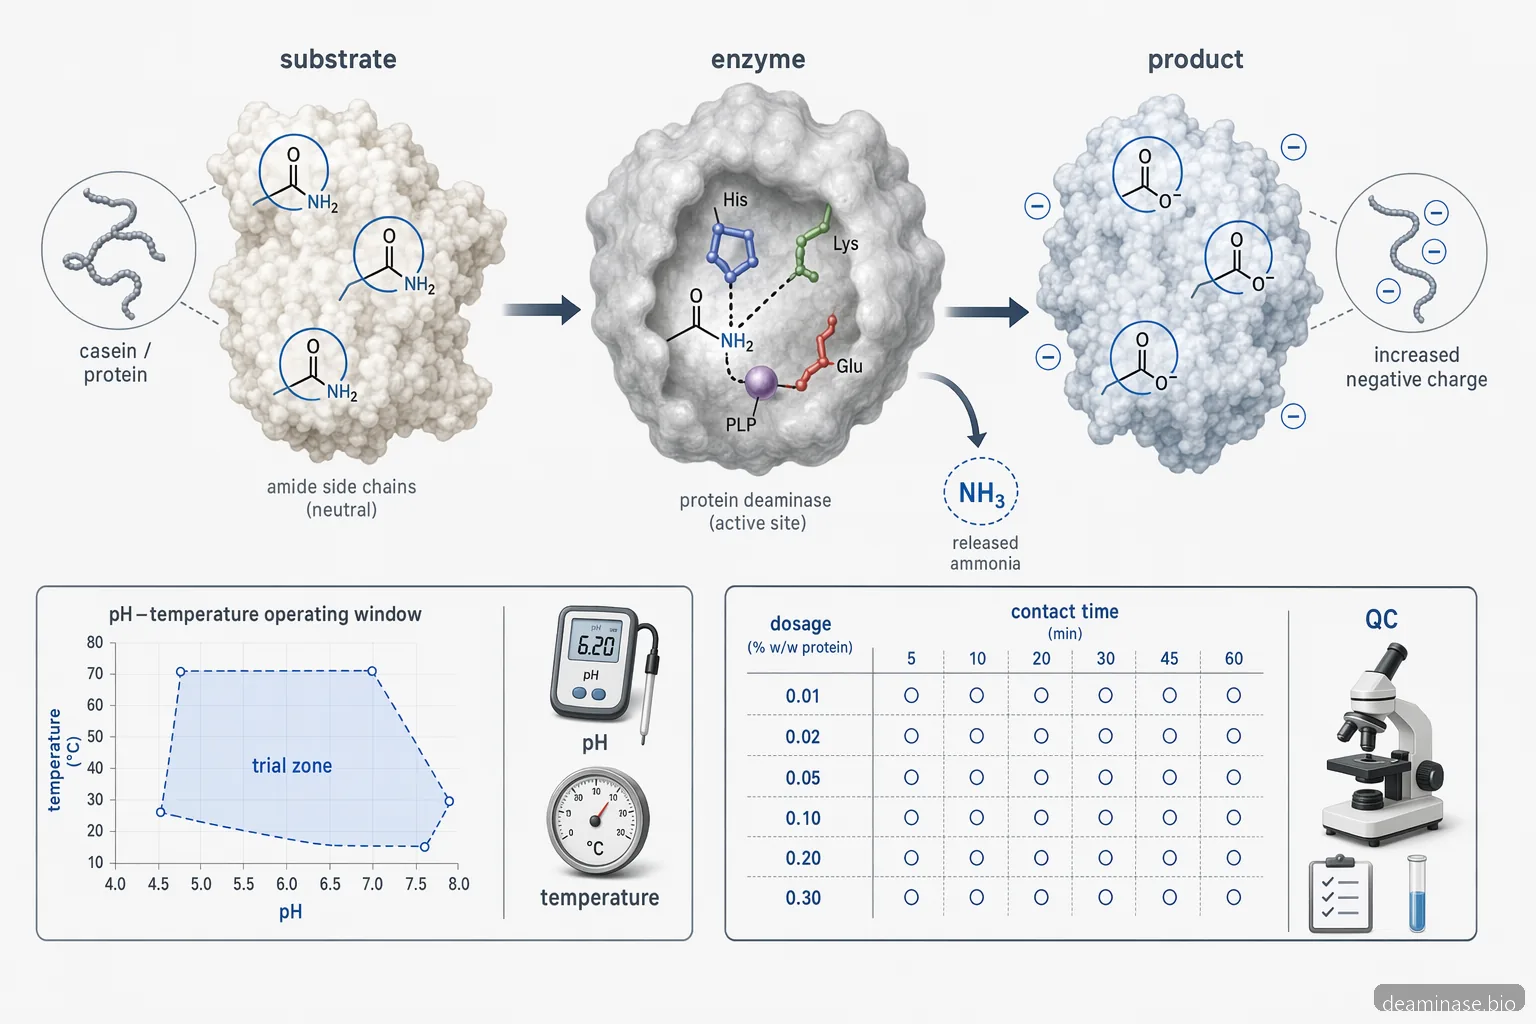
Designing the Pilot: Dose, pH, Temperature and Time
Dose by enzyme activity per gram of protein, not by product weight, because activity definitions differ between products; the technical data sheet should state the assay and the dosing basis. Compare an untreated control with at least three enzyme levels and keep milk composition, heat history, starter culture, pH schedule, salt and calcium addition constant. The product specification lists an optimum of pH 5.0 to 7.0 and 40 to 55°C; confirm the working window in your own matrix, because cheese make temperatures and acidification schedules rarely sit at the enzyme's optimum. Contact time is set by the functional target, not by the clock. Over-treatment can soften the curd, slow rennet action, add savory or bitter notes or shift moisture binding beyond specification.
Dose on activity per gram of protein. • Run untreated and heat-inactivated controls. • Record contact time, pH, temperature and protein concentration. • Do not scale from lab to plant without pilot confirmation.
Troubleshooting Common Cheese Defects
When using protein deaminase for cheese, the troubleshooting question should be specific: what defect must change, and what cannot change? For poor melt in processed cheese, evaluate melt diameter, oiling-off, viscosity, and slice integrity. For weak texture, measure curd firmness, moisture, protein recovery, and fracture force. For plant-protein cheese analogues, check solubility, grittiness, emulsification, and heat stability because deamination may improve hydration but can also expose flavor limitations in the protein raw material. If coagulation slows or curd fines increase, reduce enzyme dose, shorten contact time, shift treatment after partial protein structuring, or review calcium and pH. If flavor becomes too savory, bitter, or atypical, compare lower conversion targets and verify the enzyme preparation does not introduce side activities that affect peptides, fat, or lactose.
For melt defects: test melt, viscosity, oiling-off, and stretch. • For yield defects: test moisture, fines, whey protein loss, and curd firmness. • For analogue cheese: test hydration, emulsification, grittiness, and flavor. • For process drift: verify enzyme activity, pH meter calibration, and hold temperature.
QC Checks and Enzyme Inactivation Before Scale-Up
A qualified trial documents incoming protein composition, enzyme lot number, dosage calculation, pH, temperature, time and heat treatment. Analytical QC may include degree of deamidation where available, free ammonia, soluble nitrogen, moisture, fat, salt, pH, water activity, viscosity, melt, texture profile and the microbiology your food safety plan requires; sensory review covers dairy character, bitterness, savory intensity, mouthfeel and off-notes. Inactivation should be validated under your actual thermal profile rather than assumed: pasteurization, cooking or processed-cheese heating may be enough, but the result depends on time, temperature, solids, pH and heat transfer. If there is no kill step, check residual activity and shelf-life behaviour with your quality and regulatory teams.
Track enzyme lot and activity for every trial. • Use analytical and sensory acceptance criteria. • Validate inactivation in the real product. • Run shelf-life checks before commercial release.
How to Select a Deaminase Enzyme Supplier
A deaminase enzyme supplier for cheese should support industrial validation, not only provide a sample. Request a current COA for the lot, a TDS with activity definition and application conditions, and an SDS for safe handling. Ask whether the product is positioned as protein deaminase or protein glutaminase, what substrate was used in the activity assay, and how activity varies with pH, temperature, salt, and heat exposure. For supplier qualification, review food-use suitability for the target market, allergen and carrier information, microbiological specifications, heavy metal limits where applicable, packaging, shelf life, storage conditions, and batch-to-batch activity tolerance. A strong protein deaminase supplier for cheese should also help design pilot trials, interpret functional data, and provide scale-up guidance for dairy, plant protein, noodles, or hybrid applications when relevant.
Request COA, TDS, SDS, allergen statement, and storage guidance. • Confirm the activity assay and dosage basis. • Ask for pilot support and batch consistency data. • Evaluate cost-in-use, not only price per kilogram.
Cost-in-Use, Pack Sizes and Wholesale Quotes
Compare cost per metric ton of finished cheese, not price per kilogram of enzyme. A product with higher verified activity can cost more per kilogram and still be cheaper in use if the dose or hold time is lower. Include tank holding time, heating or cooling, yield change, rework reduction, added testing and inactivation in the calculation. The powder is packed in 1 kg, 5 kg and 25 kg fiber drums, which covers pilot work and production orders; pricing and freight are quoted per order. For a quote, send the product and activity grade, the quantity (kg or drums, one-off or recurring), the destination country, the cheese type or protein stream you will treat and the defect you want to change. Distributors and resellers supplying cheese plants are welcome to ask for recurring-volume quotes.
Compare cost per ton of finished cheese. • Include holding time, yield impact and inactivation. • Send product, quantity, destination and application with every inquiry.
Technical Buying Checklist
Buyer Questions
In cheese systems, protein deaminase modifies glutamine residues in proteins to glutamic acid residues. This can alter protein charge, hydration, emulsification, and calcium interaction. The result may affect melt, texture, moisture binding, and process consistency. Performance depends on the cheese type, protein source, pH, temperature, contact time, and enzyme dosage, so processors should validate effects in controlled pilot trials.
In food protein modification both names describe enzymes that deamidate glutamine residues in proteins to glutamic acid residues. Do not assume all products are equivalent: compare the activity assay, substrate specificity, recommended pH and temperature and the food-use documentation before you approve a product for cheese.
Start from the activity-based recommendation on the technical data sheet, expressed per gram of protein. Compare a blank control with low, medium and high levels and pick the lowest level that reaches the target. Because activity units differ between products, never convert a dose by weight alone; we give substrate-specific dosing guidance with the quotation.
Yes, it can if the treatment changes casein charge, calcium interaction, or protein hydration before renneting. Possible effects include slower coagulation, softer curd, or more fines. If this occurs, reduce dosage, shorten contact time, treat a different protein stream, adjust calcium and pH, or move the enzyme step after the most sensitive coagulation stage. Pilot trials should measure curd firmness and whey losses.
Inactivation should be validated under the actual thermal profile used in your process, not assumed from a generic temperature statement. Test residual activity where practical, or compare functional stability before and after heating during storage. Pasteurization, cooking, and processed cheese heating steps may be sufficient, but the result depends on time, temperature, matrix solids, pH, and equipment heat transfer.
A qualified supplier should provide a COA for the delivered lot, a TDS with activity definition and operating conditions, and an SDS for handling. Buyers should also request allergen and carrier information, food-use suitability for the target market, microbiological specifications, storage conditions, shelf life, packaging details, and batch-to-batch activity tolerance. These documents support supplier qualification and production traceability.
Send the product and activity grade, the quantity (kg or number of drums, one-off or recurring), the destination country, the cheese type or protein stream and the defect you want to change. Pack sizes are 1 kg, 5 kg and 25 kg fiber drums; pricing and freight are quoted per order.
Protein-Glutaminase (Protein Deaminase) for Research & Industry
Need Protein-Glutaminase (Protein Deaminase) for your lab or production process?
ISO 9001 certified · Food-grade & research-grade · Ships to 80+ countries
Frequently Asked Questions
What does deaminase enzyme do in cheese processing?
In cheese systems, protein deaminase modifies glutamine residues in proteins to glutamic acid residues. This can alter protein charge, hydration, emulsification, and calcium interaction. The result may affect melt, texture, moisture binding, and process consistency. Performance depends on the cheese type, protein source, pH, temperature, contact time, and enzyme dosage, so processors should validate effects in controlled pilot trials.
Is protein deaminase the same as protein glutaminase?
In food protein modification both names describe enzymes that deamidate glutamine residues in proteins to glutamic acid residues. Do not assume all products are equivalent: compare the activity assay, substrate specificity, recommended pH and temperature and the food-use documentation before you approve a product for cheese.
What dosage should we start with for deaminase enzyme for cheese?
Start from the activity-based recommendation on the technical data sheet, expressed per gram of protein. Compare a blank control with low, medium and high levels and pick the lowest level that reaches the target. Because activity units differ between products, never convert a dose by weight alone; we give substrate-specific dosing guidance with the quotation.
Can protein deaminase interfere with rennet coagulation?
Yes, it can if the treatment changes casein charge, calcium interaction, or protein hydration before renneting. Possible effects include slower coagulation, softer curd, or more fines. If this occurs, reduce dosage, shorten contact time, treat a different protein stream, adjust calcium and pH, or move the enzyme step after the most sensitive coagulation stage. Pilot trials should measure curd firmness and whey losses.
How do we confirm the enzyme is inactivated in a cheese process?
Inactivation should be validated under the actual thermal profile used in your process, not assumed from a generic temperature statement. Test residual activity where practical, or compare functional stability before and after heating during storage. Pasteurization, cooking, and processed cheese heating steps may be sufficient, but the result depends on time, temperature, matrix solids, pH, and equipment heat transfer.
What documents should an industrial deaminase enzyme supplier provide?
A qualified supplier should provide a COA for the delivered lot, a TDS with activity definition and operating conditions, and an SDS for handling. Buyers should also request allergen and carrier information, food-use suitability for the target market, microbiological specifications, storage conditions, shelf life, packaging details, and batch-to-batch activity tolerance. These documents support supplier qualification and production traceability.
What should we send to get a wholesale quote?
Send the product and activity grade, the quantity (kg or number of drums, one-off or recurring), the destination country, the cheese type or protein stream and the defect you want to change. Pack sizes are 1 kg, 5 kg and 25 kg fiber drums; pricing and freight are quoted per order.
Ready to source?
Turn This Guide Into a Supplier Brief Request a technical consultation and pilot sample for industrial protein deaminase cheese trials.
Contact Us to Contributehello@mail.deaminase.bio